Industries
Where our cylinders and presses work every day.
Our services
Hydraulic engineering from drawing to dispatch
We design, machine, assemble and test every system under one roof, so one team answers for it from the first drawing to the final pressure test.
- (01)
Custom cylinder design
Bore, stroke, mounting and seals specified to your load, speed and duty cycle, with drawings for your approval.
Tie-rod, welded and telescopic
- (02)
Precision machining
Barrels honed and rods ground and chromed in-house, so every tolerance is held by the people who assemble the part.
CNC turning, honing and grinding
- (03)
Power pack assembly
Motor, pump, valves and tank built as one tested unit and wired to your control panel before it ships.
Standard and custom circuits
- (04)
Repair and reconditioning
Worn cylinders stripped, measured, re-sealed and re-tested, with a report on what was found and replaced.
Collection from your site on request
Inside the works
Machined, assembled and tested under one roof
Every rod, gland and end cap is turned and finished in our own shop before a cylinder is built.
Reconditioning
Worn parts, brought back to spec
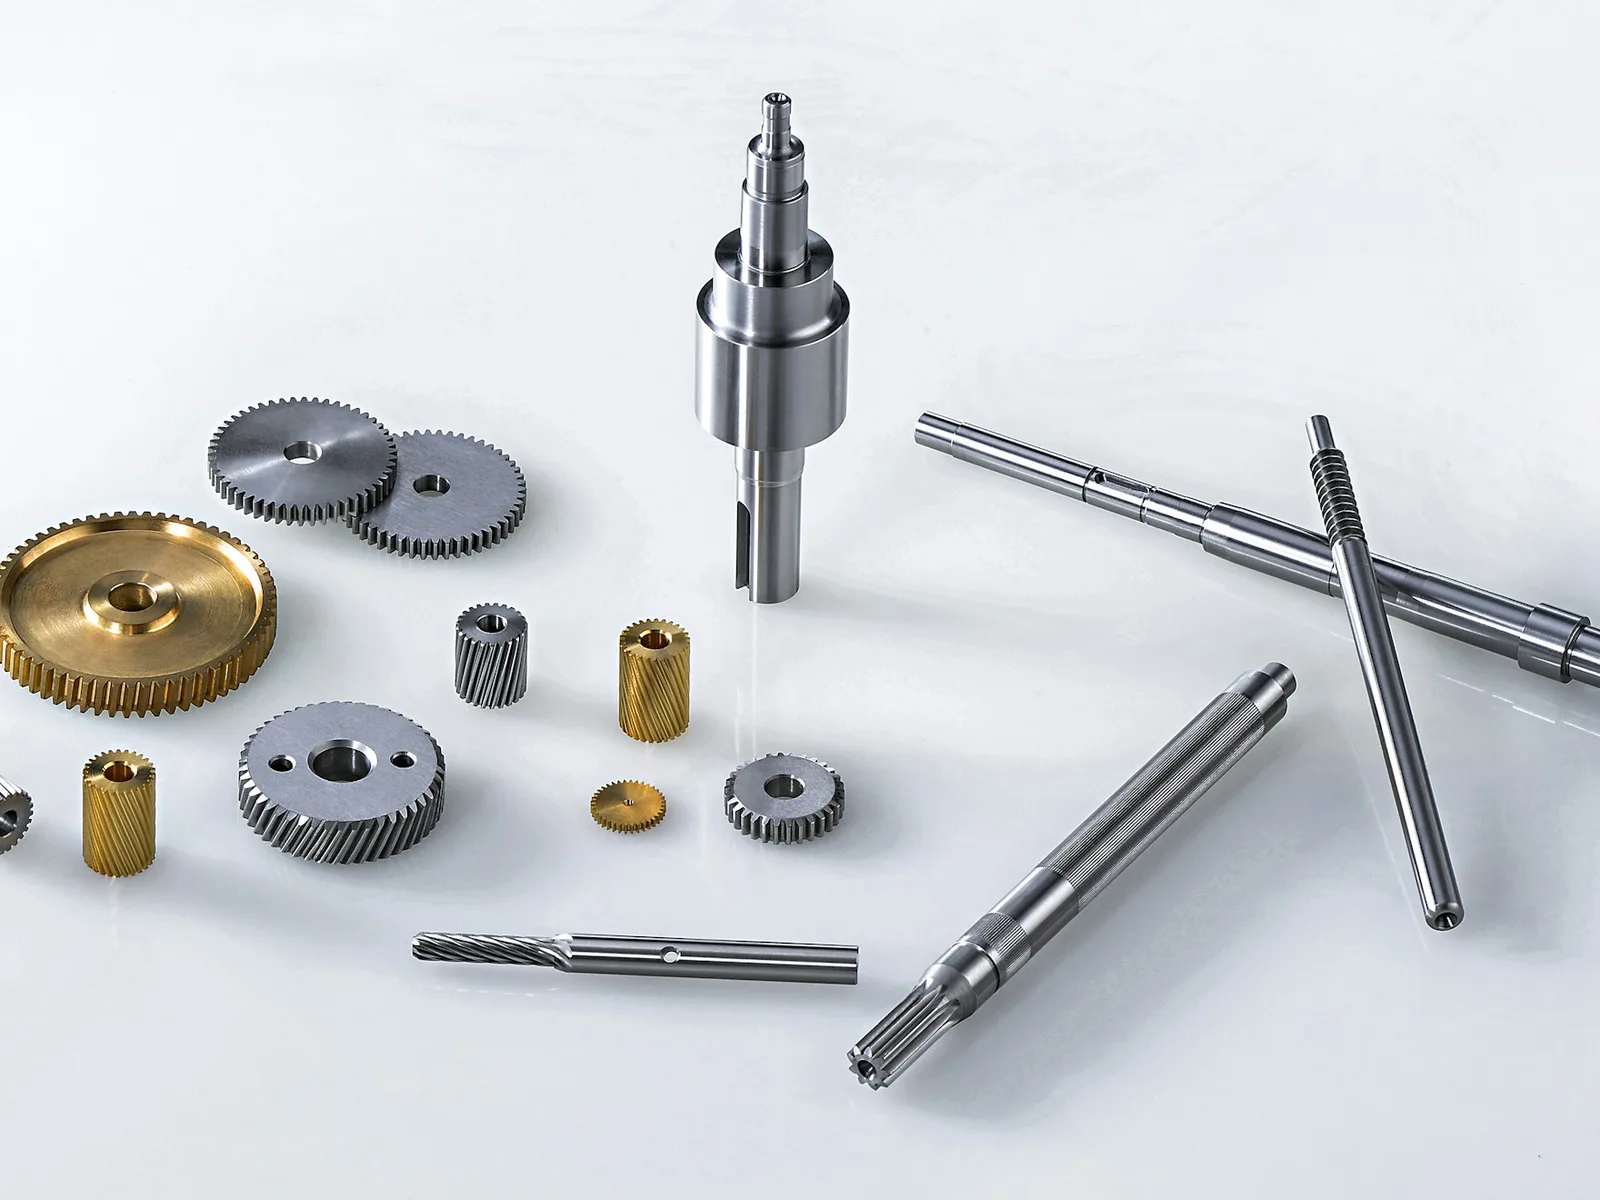
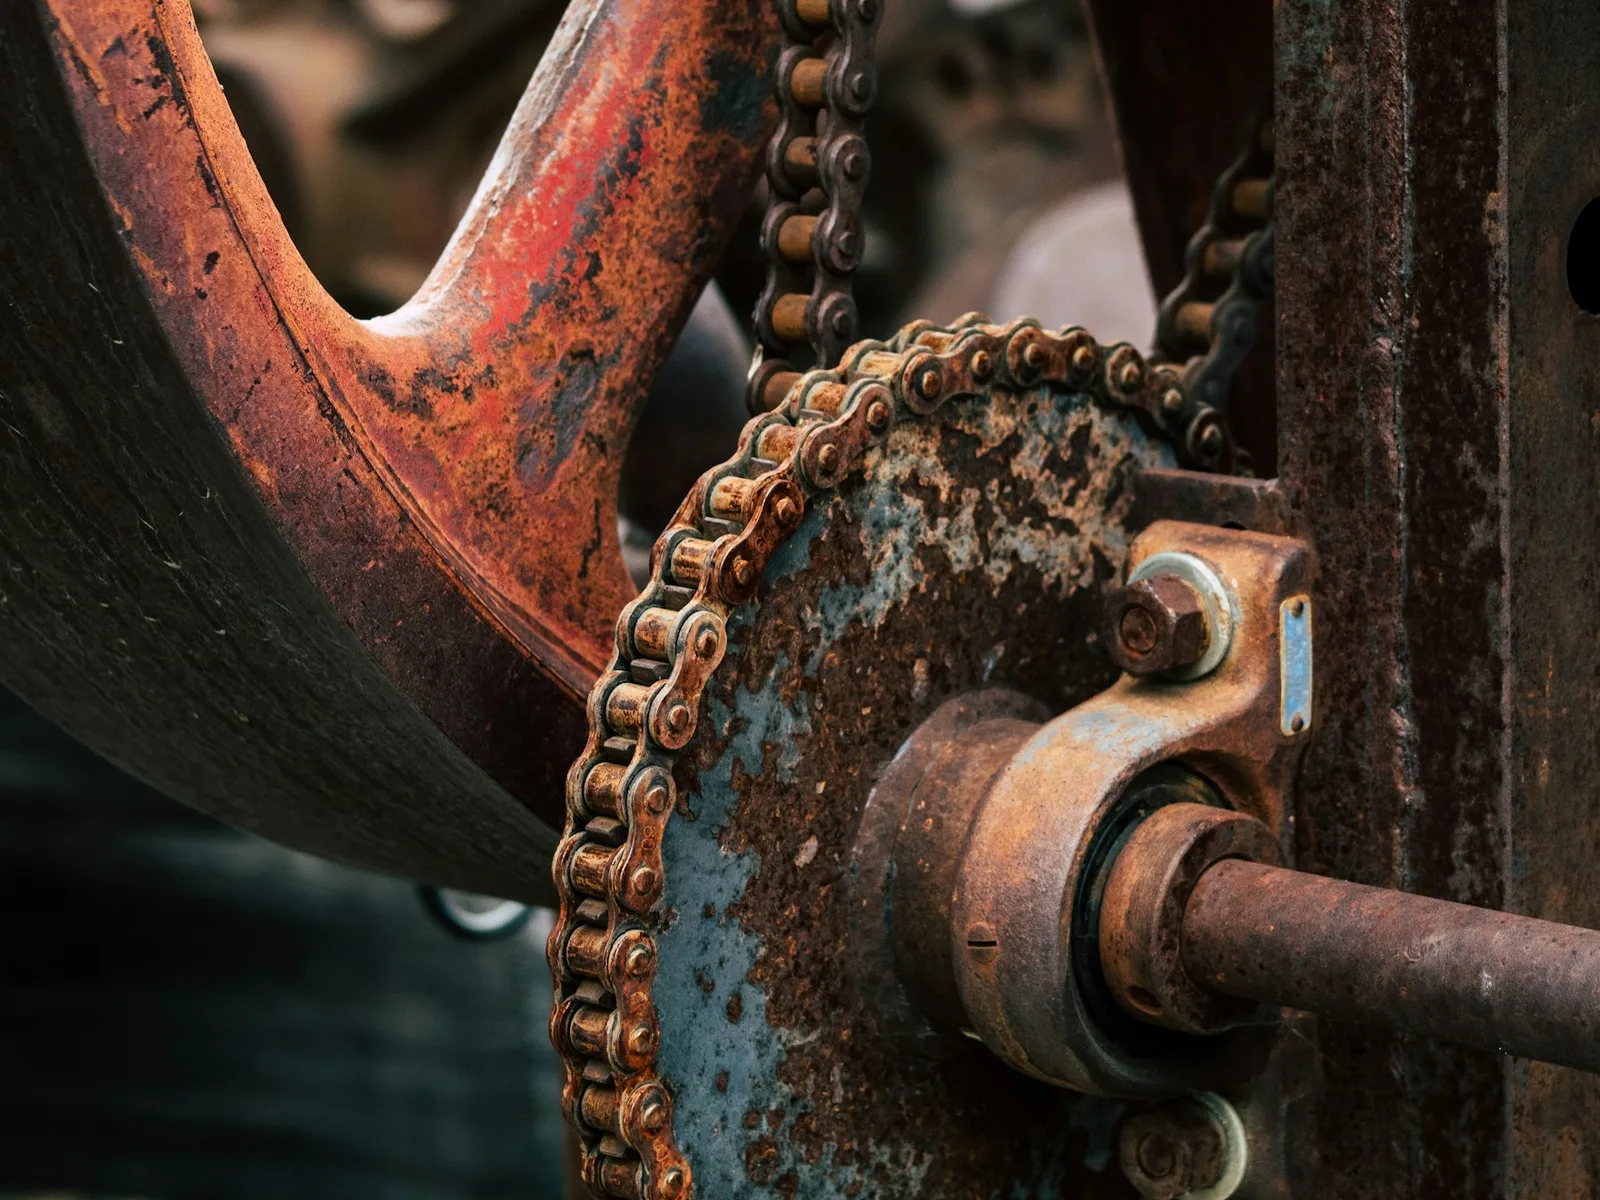
Seized drives, pitted rods and tired housings come back to us to be rebuilt. Drag the handle to see the difference.
 BeforeAfter
A seized drive, rebuilt
The corroded sprocket and shaft replaced with new ground shafts and cut gears.
 BeforeAfter
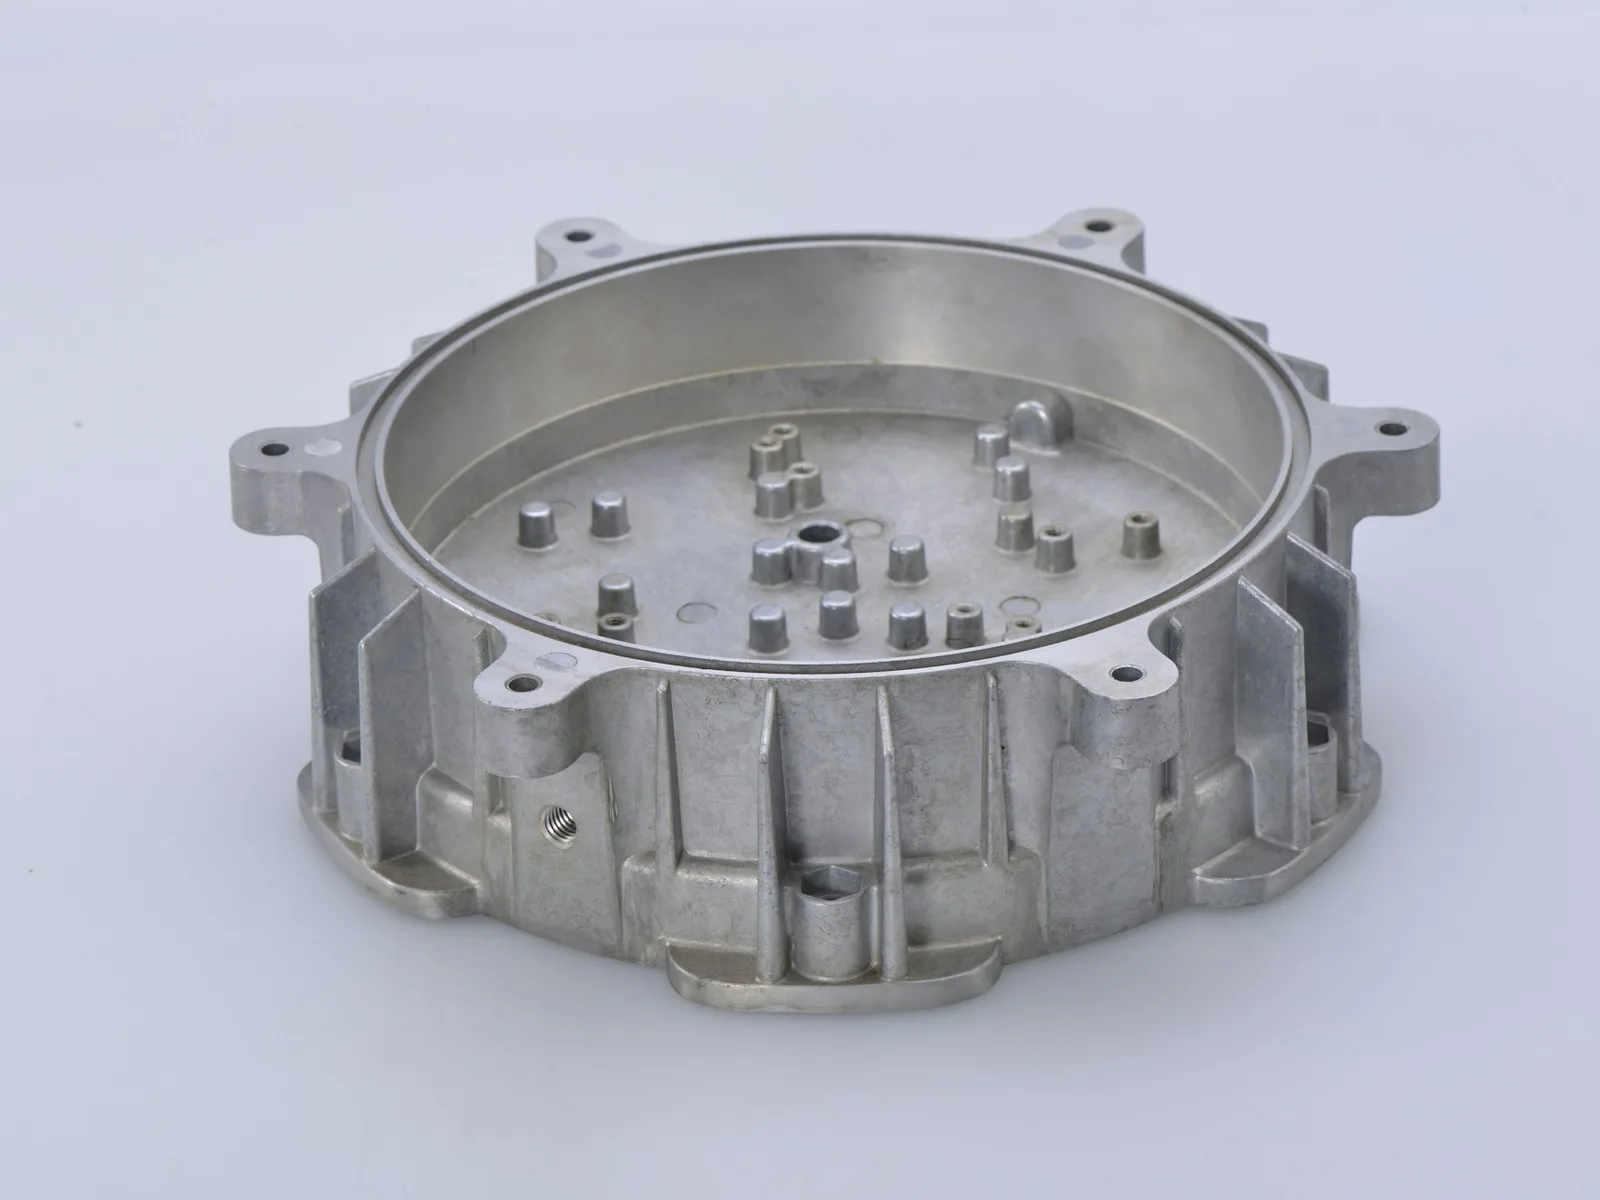
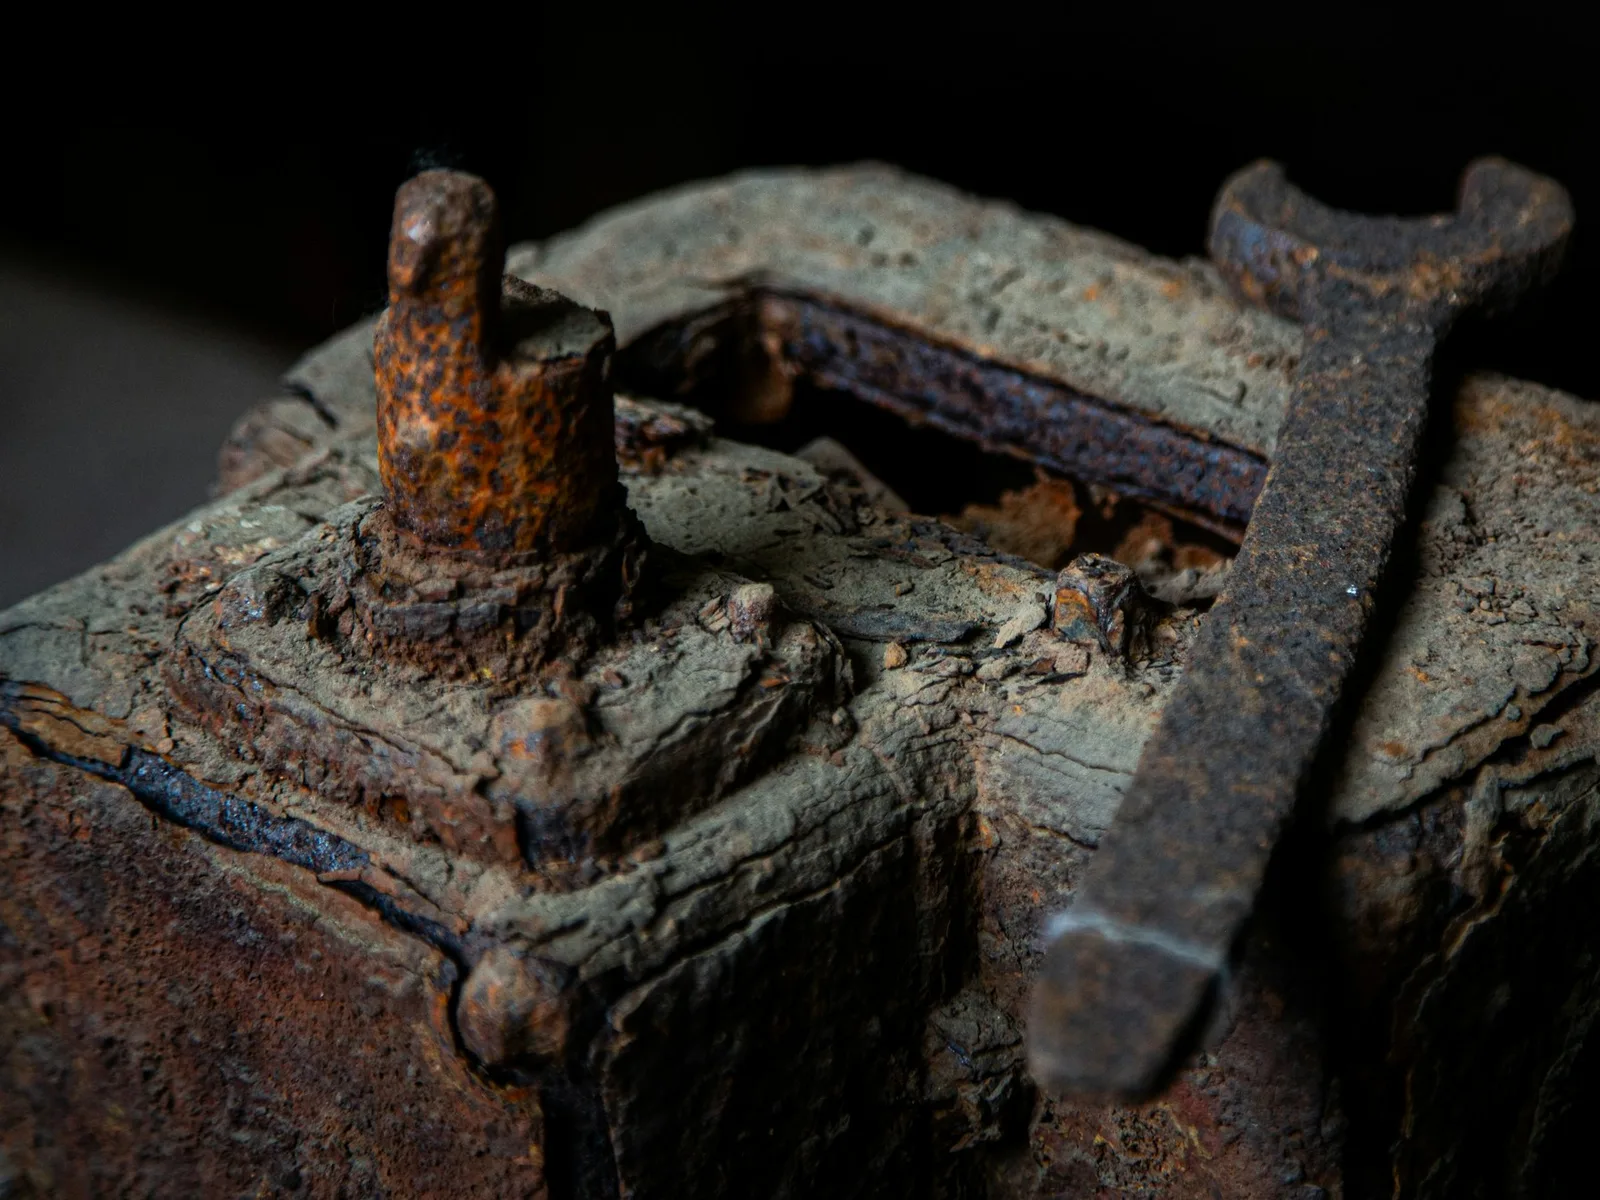
A housing, made new
A corroded block replaced by a clean casting, machined and checked.
Inside the works
Two minutes on the shop floor
From turning the rod to the final pressure test — how every cylinder is built and checked before it leaves us.
Request a quote